Moulded plastic parts · Linhai, Taizhou, Zhejiang
Out of the dust cloud, with colour dosing left unattended
Before and after
All 15 moulding machines at this plant run MegaColor units — 11 standard, 2 dual-powder and 2 dual-material. The figures below are this plant’s own.
| Measure | Before | After |
|---|---|---|
| How colour was added | Pigment weighed, resin tipped in and blended by hand | Dosed automatically to a set recipe |
| Airborne pigment | Blending in the open; dust everywhere | Fully sealed mixing chamber; no dust raised at the dosing step |
| Blending station | Staffed continuously | Unattended |
| Pigment losses | Spillage on weighing and residue in the drum, about 15% | Mixes only what the press is about to shoot, so nothing is left over — about 2% |
| Leftover resin losses | Every batch over-prepared in case it ran short, about 1.5%, with the remainder eventually sold as scrap | 0.01% (material utilisation 99.99%) |
| Blending operators | 4 | 1, covering purging, changeover and inspection |
| Monthly labour cost | RMB 36,000 (4 × RMB 9,000, including social insurance and overhead) | RMB 9,000 |
| Annual labour cost | RMB 432,000 | RMB 108,000 |
| Item | Basis | Per year |
|---|---|---|
| Labour | Blending operators from 4 to 1 at RMB 9,000 a month each, including social insurance and overhead | RMB 324,000 |
| Pigment losses | 1,000 t of resin a year at a 0.4% let-down (100 g of pigment per 25 kg of resin) needs 4 t net. With losses down from 15% to 2%, purchasing falls from 4.706 t to 4.082 t | RMB 75,000 |
| Leftover resin | Over-preparation down from 1.5% to 0.01%, about 15 t less prepared, valued at the RMB 7,000/t gap between virgin resin and scrap | RMB 104,300 |
| Total annual saving | — | about RMB 503,000 |
| Investment | 15 machines: 11 standard, 2 dual-powder, 2 dual-material | RMB 300,000 |
| Payback | Against the RMB 503,000 annual saving | about 7 months |
Where the pigment figure comes from. At 1,000 t of resin a year and 100 g of pigment per 25 kg of resin, net pigment demand is 4 t. With 15% losses they had to buy 4.706 t to cover it; at 2% losses, 4.082 t is enough. That is 0.624 t less bought each year, and at this plant’s pigment price (RMB 12 per 100 g, so RMB 120,000 a tonne) it comes to about RMB 75,000.
The resin figure is a different thing. When blending by hand you prepare a little more than the order needs in case you run short — here about 1.5%, so roughly 15 t a year. That surplus is only usable if an identical colour comes round again; otherwise it sits in a corner of the works, nobody wants to dig through it, and in the end most of it goes out as scrap. So the loss is not the full value of the resin, it is the gap between the virgin price and the scrap price: virgin PP at RMB 8,000 a tonne against RMB 1,000 a tonne as scrap, a gap of RMB 7,000. Fifteen tonnes at that gap is RMB 105,000. After the retrofit this falls to 0.01% (material utilisation 99.99%), a net saving of RMB 104,300. The machine can also be set to stop after a given number of doses — work out how many an order needs, set it, and the machine stops itself, so in principle a batch is never over-prepared.
These are two separate accounts. The first covers losses of the pigment itself — spilled on weighing, left in the bottom of the drum. The second covers batches of resin prepared in excess and sold as scrap. Different material, different point in the process, so they are listed separately. Note also that those 15 t of surplus contained about 60 kg of pigment which is not counted here, so the figure is on the conservative side.
Do not treat this plant’s numbers as your forecast. Labour, loss rates and payback all follow directly from how many machines you run, what you make and which pigments you use. This is a 15-machine plant getting through 1,000 t of resin a year; your situation is different and so is the answer. To get your own, work through the calculator with your actual figures, or send them to us and we will do it with you.
How it happened
Anyone who has blended colour by hand knows the scene: open the pigment sack and it is in the air. Operators in masks, fans running, and a film of it over the floor, the machines and the people. It is not only a housekeeping problem — pigment drifting to the next station is how the following light-coloured batch gets contaminated.
The point of the retrofit here was not to save a few operators, it was to close the whole step in. Pigment goes into a sealed tank, the gear meters it inside a sealed cavity, and the mixing chamber blends only what the press is about to shoot and feeds it straight into the barrel. From sack to machine nothing is opened and nothing hits the floor.
The immediate result is that nobody has to stand at the blending station. The operators who were blending now inspect instead, and no longer work in pigment dust. What that improvement in conditions does for hiring and retention, the customer can tell you better than we can.
We present this case alongside the bottle-cap plant in Yuyao: one makes the financial argument, the other the argument about conditions and process. Together they are the full reason to change.
That blending station used to sit inside a cloud of dust. Now the job does not need anyone at all.
Quoted from MegaColor’s own account of this installation. We identify customer plants by city and industry only.
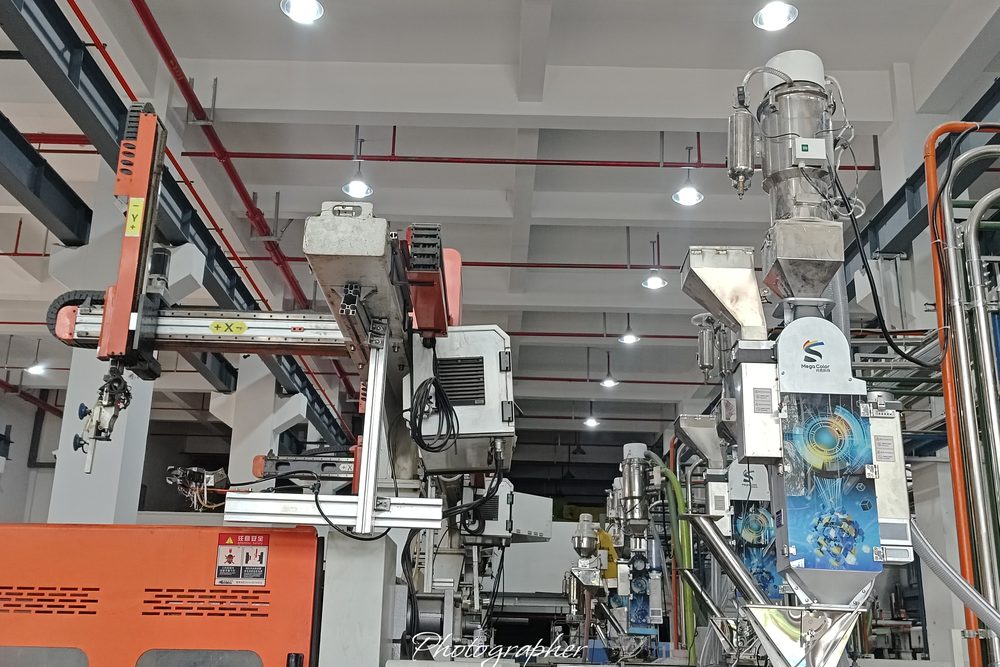
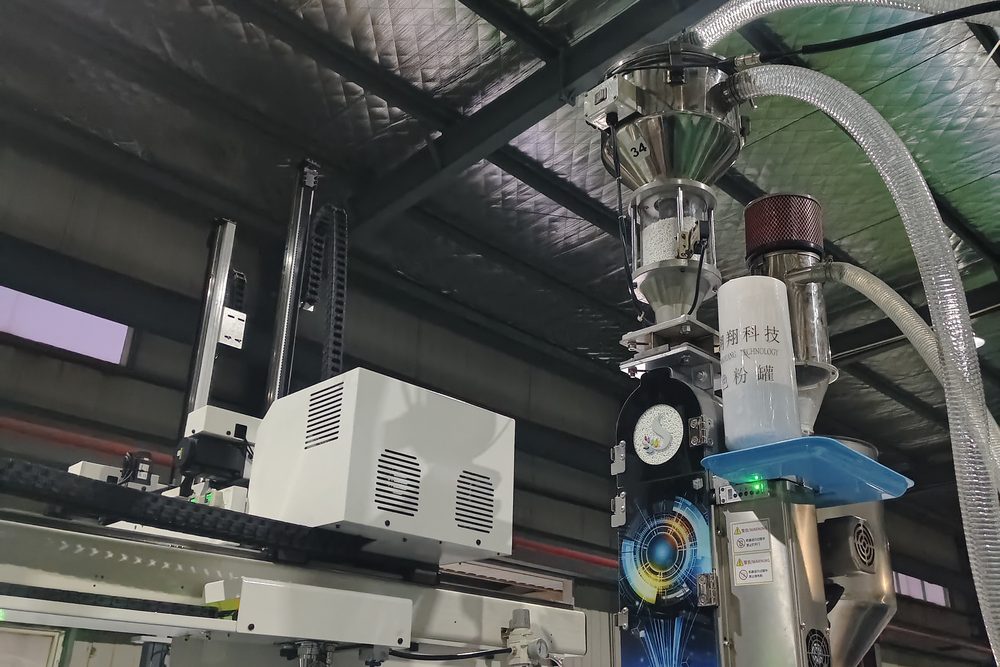
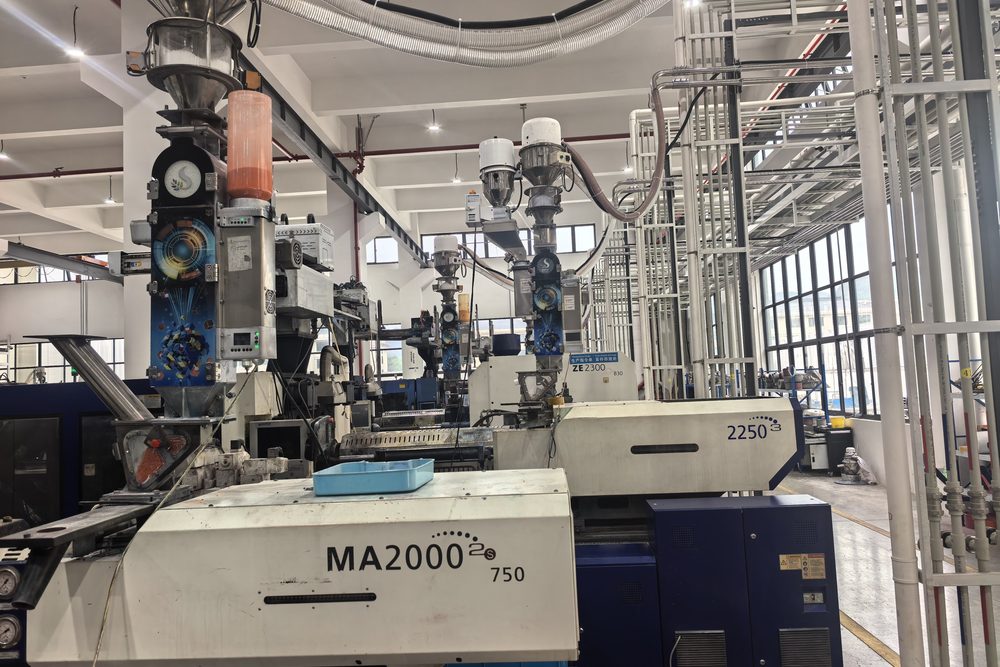
Photographs from the floor
Photographs from customer plants. At their request these show the equipment and the work station only — no company names, signage or anything that identifies the site.
Who this case applies to
Close enough to read across directly
- Plants still opening sacks and blending by hand, with pigment in the air
- Light-coloured or clear parts at risk of cross-contamination from drifting pigment
- Sites under pressure from environmental or occupational-health inspection
- A blending role you cannot fill or cannot keep filled
Different enough that you should not read the figures across
- Plants already on enclosed conveying — there is little left to gain on conditions
- If payback is all you want to see, read the bottle-cap moulder in Yuyao
- Running high-temperature resins → see the high-temperature models
Do not treat somebody else’s numbers as your forecast. Labour, reject rate and payback all depend heavily on how many moulding machines you run, how often you change colour, and how the work is staffed today. The same machine in two different plants can save amounts that differ several times over. To get your own figure, tell us your machine count, your shift pattern and how often you change colour — or just send material for a trial.
Want to know how it runs on your material?
Somebody else’s case is a reference point; the data from your own material is what you can decide on. Send it to us for a trial run — there is no charge for this.
For a trial we need the resin grade, the pigment reference and the let-down ratio. Results normally come back within 3 working days.